| Brand Name: | OEM |
| Model Number: | QJB |
| MOQ: | 2 |
| Price: | 1000-5000USD |
| Payment Terms: | TT |
| Supply Ability: | 100 PCS PER MONTH |
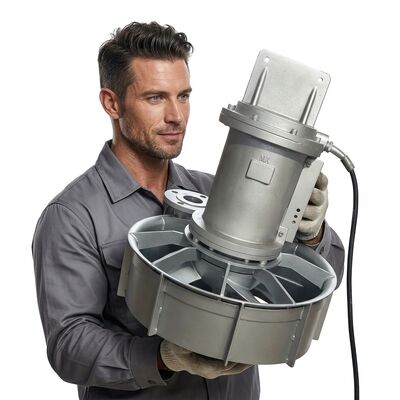
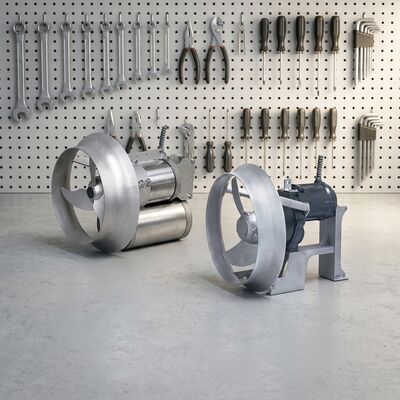
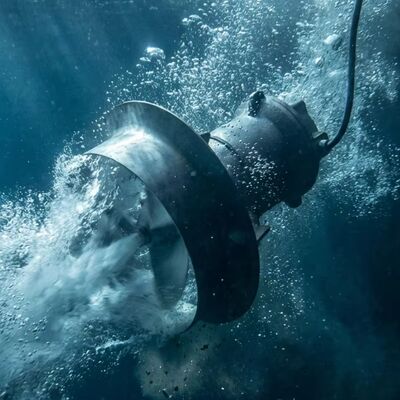
The Submersible Mixer Pump is a highly efficient and robust piece of equipment designed for various industrial and municipal applications. Engineered to deliver superior mixing performance, this pump is ideal for use in wastewater treatment plants, sludge processing, and other fluid agitation tasks. Constructed with high-quality materials such as cast iron and stainless steel (SS), the submersible mixer pump ensures durability, corrosion resistance, and long service life even in the most demanding environments.
One of the standout features of this submersible mixer pump is its insulation class F, which guarantees excellent thermal resistance and reliability under continuous operation. This insulation class allows the motor to withstand higher temperatures, thereby enhancing the pump's operational safety and efficiency. Such a feature is crucial for applications where the pump runs for extended periods without interruption.
With a power rating range from 0.37 kW to 22 kW, the submersible mixer pump offers versatile options to meet varying operational needs. Whether the requirement is for small-scale mixing or large-scale agitation, this pump can be tailored to provide the appropriate power output. This flexibility makes it suitable for a broad spectrum of industries, including chemical processing, food and beverage and environmental management.
The pump’s protection grade is IP68, ensuring complete protection against dust ingress and allowing for continuous submersion in water or other fluids. This high degree of protection makes the submersible agitator an excellent choice for harsh and wet conditions, where reliability and safety are paramount. Operators can trust that the pump will perform consistently without the risk of damage due to water ingress, which is essential for submerged applications.
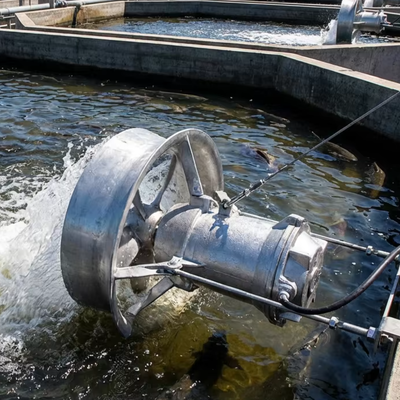
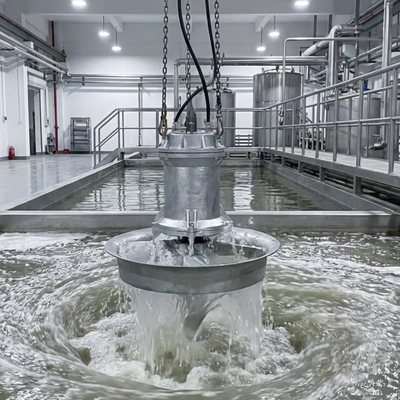
The submersible mixer pump is designed to provide efficient mixing and agitation by creating a powerful flow within tanks or basins. This flow helps to keep solids in suspension, improve chemical reactions, and enhance the overall treatment process in wastewater facilities. Its compact and sealed design allows it to be installed directly into the fluid, eliminating the need for additional shafts or bearings exposed to the liquid, thereby reducing maintenance requirements and downtime.
Another advantage of this submersible agitator is its ease of installation and operation. The pump can be quickly submerged into the desired location and connected with minimal effort, making it convenient for both new installations and retrofitting existing systems. Its robust construction and reliable motor design minimize the need for frequent repairs, contributing to lower operating costs over time.
In summary, the Submersible Mixer Pump is a state-of-the-art solution for fluid mixing and agitation needs. Its cast iron or stainless steel construction ensures strength and corrosion resistance, while the insulation class F and IP68 protection grade guarantee reliable and safe operation under harsh conditions. With a wide power rating range from 0.37 kW to 22 kW, this submersible mixer pump can be adapted to various industrial applications, making it an indispensable tool for efficient and effective fluid management.
Whether you require a submersible mixer pump for wastewater treatment, sludge agitation, or any other process that demands reliable mixing performance, this product offers the durability, power, and protection you need. Investing in this submersible agitator means choosing a dependable and long-lasting solution that enhances operational efficiency and reduces maintenance challenges.
| Product Name | Submersible Mixer Pump |
| Application | Industrial |
| Power Rating | 0.37-22kW |
| Power Source | Electric |
| Material | Cast Iron / SS |
| Cable Length | 10m |
| Protection Grade | IP68 |
| Insulation Class | F |
| Warranty | 1 Year |
The OEM Submersible Mixer Pump, model number QJB, originating from Zhejiang Province, Quzhou, is a highly reliable and efficient solution designed for a wide range of industrial and municipal applications. Certified with ISO9001, this submersible agitator is engineered to deliver exceptional performance in demanding environments, ensuring durability and long service life. With a power rating ranging from 0.37 to 22kW and an insulation class F, the pump is suitable for continuous operation in various liquid mixing and agitation scenarios.
This submersible mixer pump is ideal for wastewater treatment plants, where it is commonly used for mixing sludge and preventing sedimentation in tanks and basins. Its IP68 protection grade ensures complete waterproofing and dust resistance, making it perfect for submerged operation in harsh conditions. The 10-meter cable length allows flexible installation depths and easy integration into existing systems. The pump's robust design and plywood packaging ensure safe delivery within 10-15 days, meeting the supply ability of 100 pieces per month.
In addition to municipal sewage treatment, the submersible agitator is widely used in agricultural irrigation, aquaculture, and industrial processes such as chemical mixing, pulp and paper mills, and food processing plants. Its ability to provide thorough mixing and maintain homogeneity in liquids makes it indispensable for these industries. The submersible mixer pump prevents stratification and enhances the efficiency of biological treatment by maintaining optimal conditions for microorganisms.
With a minimum order quantity of 2 units and a price range of 1000-5000 USD, the OEM Submersible Mixer Pump offers excellent value for businesses seeking reliable mixing solutions. Payment terms are flexible with TT accepted, ensuring smooth transactions. The pump’s sturdy construction, coupled with its superior performance as a submersible agitator, makes it a preferred choice for engineers and procurement managers looking for dependable equipment that guarantees operational stability and efficiency.
Overall, the OEM submersible mixer pump is a versatile and efficient agitator solution designed to meet the needs of various application occasions and scenarios, ensuring optimal mixing performance, durability, and ease of maintenance in submerged conditions.
Our Submersible Mixer Pump is designed for reliable and efficient mixing in wastewater treatment, sludge handling, and other industrial applications. To ensure optimal performance, please follow the installation and maintenance guidelines provided in the product manual.
For technical support, our team of experts is available to assist with troubleshooting, product setup, and operational advice. We recommend regular inspection and cleaning of the mixer pump to prevent buildup and ensure longevity.
Spare parts and replacement components are available to maintain the product’s performance. We provide comprehensive service options including installation support, routine maintenance, and repair services to minimize downtime and extend the life of your equipment.
For detailed technical documentation, including installation manuals, wiring diagrams, and performance curves, please refer to the product resources section on our website.
We are committed to providing timely and effective support to help you maximize the efficiency and reliability of your Submersible Mixer Pump.